
Common Defects Found in High Volume Runs & How to Prevent Them
Comments Off on Common Defects Found in High Volume Runs & How to Prevent ThemClick to Expand

Avoiding defects is a major goal in metal stamping. Over time, machinery needs recalibration, and punches and tools need sharpening or realignment. If these issues are ignored, stampings may drift out of tolerance, leading to extra time and money for rework.
Your stamping partner should value quality control as much as you do. At Keats Manufacturing, we are always watching for defects and out-of-tolerance stampings during manufacturing and with specialized inspection methods. Keep reading to learn more.
Defect Rates
In small production runs, it’s often possible to inspect individual stampings manually – this is not so much the case at high volumes. Defect rates can soar if problems are not fixed early. Stampers turn to inspection methods that use computers and automation to find defects and errors while maintaining efficiency.
One option is coordinate measuring machines or CMMs. These devices use delicate probes or vision cameras to physically or optically assess a part’s dimensions and features. By comparing the part against stored coordinate data or a digital image, CMMs identify when a part is out of tolerance.
To speed up the process, specialized fixturing is used to position multiple parts for inspection at once. This helps operators maintain their workflow while incorporating quality control.
Forming and Dimensional Defects
Forming and dimensional defects can occur as a result of the material used, worn or improperly assembled tooling, or design problems like defect-prone part features or specifications that are challenging to achieve.
Defects or problems that appear repeatedly signal a stamping error. Identifying and resolving them quickly makes it easier to avoid scrap and rework and minimizes the risk of defective parts reaching you or your customers.
Forming Defects
Metal forming is the process of changing the shape of a metal workpiece without adding or removing material. Common examples of forming defects include:
- Cracking and tearing
- Galling or scratching
- Misalignment or shifting inside the press
- Incorrect punch or guide angles
Dimensional Defects
Metal stamping involves changing the shape of a workpiece by cutting, punching, shearing, blanking, or otherwise removing material to create a finished part. Defective parts are often out of tolerance, which affects their fit and function in an assembly or finished product.
Common sheet metal stamping defects include:
- Twisting, wrinkles, or improper flatness
- Incorrect hole placement, size, or shape
- Incorrect bend angles or springback
- Burrs and deformed edges
- Overall part length/width defects
Stamping defects are often caused by a misaligned material feed, worn or broken punches, material defects, improper force or tonnage, or other problems.
Packaging Defects
Packaging mistakes can also lead to damaged parts, scrap and rework, fulfillment delays, and extra expenses.
Incorrect or Missing Shipping Markings and Barcodes
Incorrect barcodes or labels in the wrong place are inconvenient in smaller orders, and it only compounds in a high-volume production run. It takes time and money to relabel dozens or hundreds of boxes and cases, or to recheck part numbers, shipping info, or dimensional details. That in turn causes fulfillment delays, so it’s critical that inspection includes checks for these errors.
Container and Product Defects
Components may be packaged manually by workers or with automated or semi-automated equipment, or even a combination. Regardless of the method, parts can be damaged if they are packed incorrectly, jostled and scratched, or if the packaging itself is damaged, bent, or torn. Some packaging methods like tape and reel encapsulation for very small parts, or custom trays to isolate individual parts, can prevent damage during packaging.
Another important step is the final inspection of packed parts. This ensures packaging is correct and no defective parts were missed in earlier inspections. It can be done by workers as they pack items or with machine vision equipment, comparing an image of a correctly packed tray or box with items as they exit the packaging line.
Metal Stamping Services From Keats Manufacturing
Errors and defects can happen at many points in the stamping and packaging process. That’s why you should work with a manufacturer who prioritizes attention to detail at every turn and has taken the steps to mitigate the risk of defects.
At Keats Manufacturing ee are ISO:9001, ISO:14001, and IATF:16949 certified. We provide high-quality metal stamping and finishing services with careful inspection and packaging to meet your needs. Contact us to learn more or request a quote to start your order.
Frequently Asked Questions
What are the most common defects Keats Manufacturing Co. detects in high volume metal stamping runs?
The most common defects Keats Manufacturing Co. detects in high volume metal stamping runs are dimensional inaccuracies, burrs, surface imperfections, and incomplete forming.
- These issues are typical examples of common defects found in high volume runs, and Keats Manufacturing Co. implements targeted prevention strategies—such as in-house quality assurance, advanced measurement systems, and automated sensor inspections—to minimize their occurrence and ensure consistent quality.
- Our in-house quality assurance teams utilize advanced measurement systems to catch deviations as small as ±0.0005 in.
- Automated sensor systems and operator inspections help identify burrs, cracks, and surface flaws during production.
- All dies and tooling are engineered and built in-house with a lifetime guarantee, ensuring consistent, defect-minimized output even at high speeds.
How does Keats Manufacturing Co. minimize dimensional defects during production?
Keats Manufacturing Co. minimizes dimensional defects—one of the most common defects found in high volume runs—by engineering every die and tool in-house and maintaining strict process controls.
- Our EDM, CNC, and CAD/CAM capabilities allow us to hold tolerances as tight as ±0.0005 in., reducing the risk of out-of-spec parts.
- Regular in-process inspections are conducted using precision measurement equipment across our 150–175 stamping and wire-forming machines.
- Lifetime tooling support ensures ongoing accuracy, even in extended high-volume runs.
What quality control methods does Keats Manufacturing Co. use to detect defects early?
Keats Manufacturing Co. uses a combination of advanced automated optical inspection systems and in-line sensor technology integrated directly with our high-speed stamping and wire forming machines—over 150–175 across our three facilities—to detect defects early in the production process.
- Real-time monitoring of critical dimensions and surface details allows us to catch even minute deviations, meeting tolerances as tight as ±0.0005 in.
- Our skilled operators also perform regular manual inspections to supplement automated checks, ensuring visual and tactile defects are identified.
- Any defective parts are immediately removed from the line, supporting our commitment to just-in-time delivery and consistently high quality standards.
Does Keats Manufacturing Co. offer guaranteed defect rates for high volume orders?
Yes, Keats Manufacturing Co. offers documented defect rate guarantees for high-volume orders.
- We engineer and build all dies and tooling in-house, backed by our lifetime guarantee, which allows us to maintain defect rates as low as 25 parts per million (PPM) on many projects.
- Our IATF certified quality management system includes real-time inspections and automated assembly lines capable of up to 200 pieces per minute, ensuring consistent quality.
- Upon request, we provide full defect rate documentation and traceability for every batch, supporting your quality and compliance requirements.
How does in-house tooling at Keats Manufacturing Co. help prevent recurring defects?
In-house tooling at Keats Manufacturing Co. helps prevent recurring defects by enabling immediate adjustments and proactive maintenance using our in-house EDM, CNC, and CAD/CAM capabilities.
- All dies and tooling are engineered and built on-site to ensure optimal compatibility with each unique part design, supporting tolerances as tight as ±0.0005 in.
- By rapidly identifying and correcting issues, our team addresses common defects found in high volume runs before they recur.
- The lifetime guarantee on our tooling means any wear or issues are resolved before they impact part quality.
- With over 150–175 stamping and wire-forming machines across three facilities, our rapid response to tooling needs keeps production running smoothly and minimizes the risk of repeat defects.
Can Keats Manufacturing Co. handle high precision requirements without increasing defect risk?
Keats Manufacturing Co. consistently achieves high precision requirements—down to ±0.0005 in.—without increasing defect risk due to our advanced equipment and quality controls.
- We operate over 150–175 state-of-the-art stamping and wire-forming machines across three facilities.
- Automated assembly and inspection systems maintain accuracy even at speeds up to 200 pieces per minute.
- To specifically address common defects found in high volume runs and how to prevent them, our experienced engineering team reviews every design for manufacturability and optimal process flow, ensuring defect risks are minimized during production.
What secondary processes does Keats Manufacturing Co. use to eliminate defects after forming?
Keats Manufacturing Co. uses a range of secondary processes to eliminate defects after forming, including deburring, degreasing, heat-treating, and powder coating.
- These secondary processes are integrated directly into Keats’ workflow, with deburring and cleaning performed in-line using specialized equipment across our three facilities to remove sharp edges and contaminants.
- Each part can be finished with plating, e-coating, or stress relieving to enhance durability and surface quality, with all tooling engineered and maintained in-house to ensure consistency.
- Our secondary services help ensure finished components meet strict tolerances as tight as ±0.0005 in. and adhere to both functional and cosmetic standards, backed by our IATF 16949:2015 certified quality system.
How does Keats Manufacturing Co. ensure consistent quality across multiple high volume production sites?
Keats Manufacturing Co. ensures consistent quality across all facilities by standardizing processes, equipment, and quality controls company-wide.
- Every site operates under the same IATF-certified systems and utilizes in-house engineered dies and tooling, which are backed by our lifetime guarantee.
- Real-time production data and inspection reports are monitored centrally for immediate issue resolution, leveraging our network of over 150–175 stamping and wire-forming machines.
- This unified approach, including just-in-time delivery and automated assembly up to 200 pieces per minute, is specifically designed to minimize common defects in high volume runs and ensure effective prevention measures are consistently applied at all three locations, delivering identical, high-quality parts.
What Is Metal Stamping?
Comments Off on What Is Metal Stamping?Click to Expand
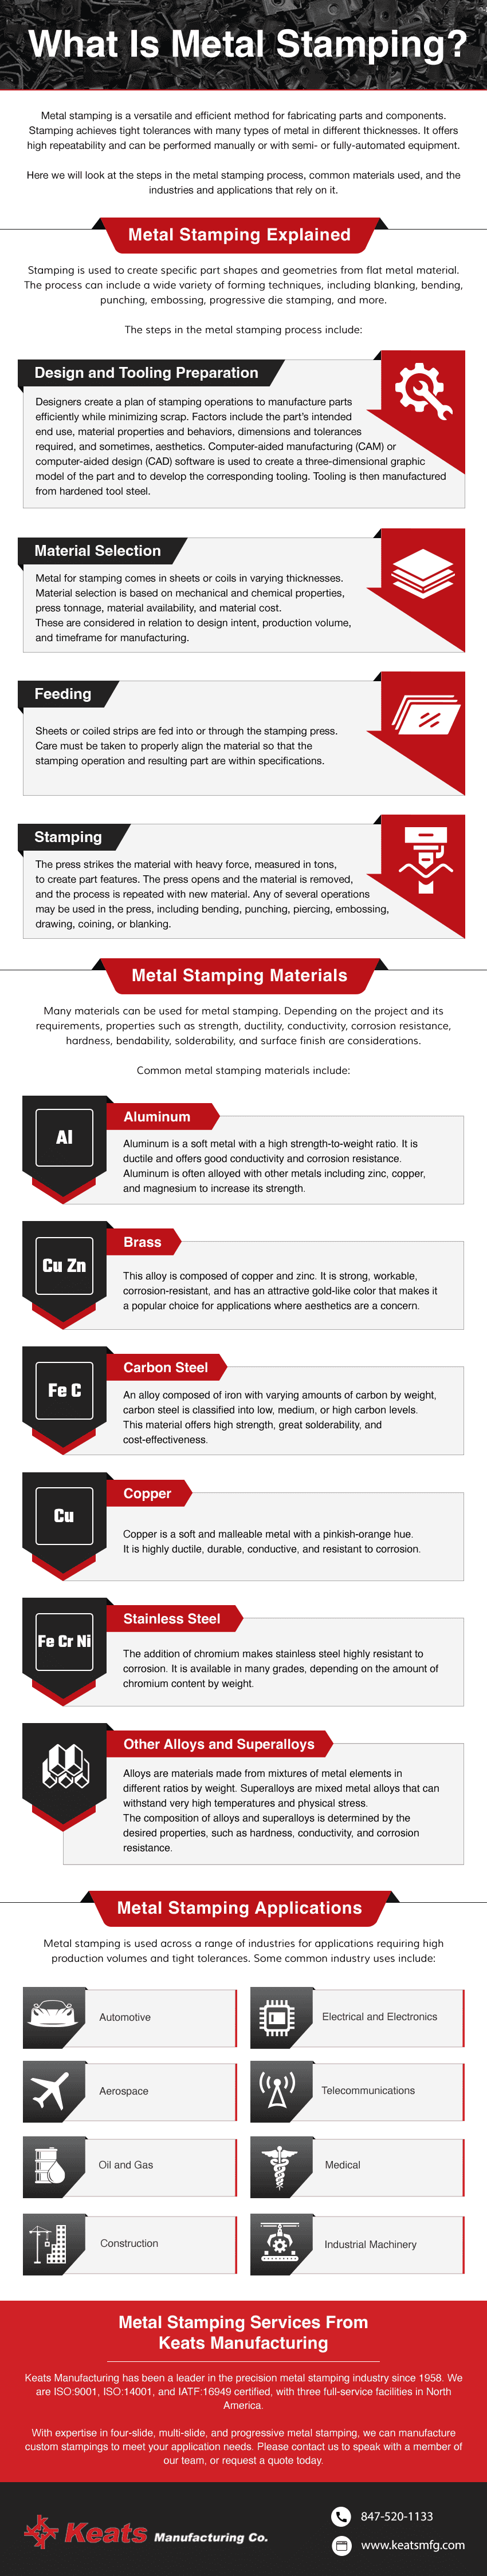
Metal stamping is a versatile and efficient method for fabricating parts and components. Stamping achieves tight tolerances with many types of metal in different thicknesses. It offers high repeatability and can be performed manually or with semi- or fully-automated equipment.
Here we will look at the steps in the metal stamping process, common materials used, and the industries and applications that rely on it.
Metal Stamping Explained
Stamping is used to create specific part shapes and geometries from flat metal material. The process can include a wide variety of forming techniques, including blanking, bending, punching, embossing, progressive die stamping, and more.
The steps in the metal stamping process include:
- Design and Tooling Preparation. Designers create a plan of stamping operations to manufacture parts efficiently while minimizing scrap. Factors include the part’s intended end use, material properties and behaviors, dimensions and tolerances required, and sometimes, aesthetics. Computer-aided manufacturing (CAM) or computer-aided design (CAD) software is used to create a three-dimensional graphic model of the part and to develop the corresponding tooling. Tooling is then manufactured from hardened tool steel.
- Material Selection. Metal for stamping comes in sheets or coils in varying thicknesses. Material selection is based on mechanical and chemical properties, press tonnage, material availability, and material cost. These are considered in relation to design intent, production volume, and timeframe for manufacturing.
- Feeding. Sheets or coiled strips are fed into or through the stamping press. Care must be taken to properly align the material so that the stamping operation and resulting part are within specifications.
- Stamping. The press strikes the material with heavy force, measured in tons, to create part features. The press opens and the material is removed, and the process is repeated with new material. Any of several operations may be used in the press, including bending, punching, piercing, embossing, drawing, coining, or blanking.
Metal Stamping Materials
Many materials can be used for metal stamping. Depending on the project and its requirements, properties such as strength, ductility, conductivity, corrosion resistance, hardness, bendability, solderability, and surface finish are considerations.
Common metal stamping materials include:
- Aluminum. Aluminum is a soft metal with a high strength-to-weight ratio. It is ductile and offers good conductivity and corrosion resistance. Aluminum is often alloyed with other metals including zinc, copper, and magnesium to increase its strength.
- Brass. This alloy is composed of copper and zinc. It is strong, workable, corrosion-resistant, and has an attractive gold-like color that makes it a popular choice for applications where aesthetics are a concern.
- Carbon Steel. An alloy composed of iron with varying amounts of carbon by weight, carbon steel is classified into low, medium, or high carbon levels. This material offers high strength, great solderability, and cost-effectiveness.
- Copper. Copper is a soft and malleable metal with a pinkish-orange hue. It is highly ductile, durable, conductive, and resistant to corrosion.
- Stainless Steel. The addition of chromium makes stainless steel highly resistant to corrosion. It is available in many grades, depending on the amount of chromium content by weight.
- Other Alloys and Superalloys. Alloys are materials made from mixtures of metal elements in different ratios by weight. Superalloys are mixed metal alloys that can withstand very high temperatures and physical stress. The composition of alloys and superalloys is determined by the desired properties, such as hardness, conductivity, and corrosion resistance.
Metal Stamping Applications
Metal stamping is used across a range of industries for applications requiring high production volumes and tight tolerances. Some common industry uses include:
- Automotive: Body panels, brackets, battery contacts, and cover plates
- Electrical and electronics: Clips, tabs, and pins for mobile phones and devices; switches, brackets, terminals, and contacts for appliances and equipment
- Aerospace: High-strength, lightweight components such as panels, cabin equipment, and other parts throughout aircraft
- Telecommunications: Switches, router components, contact plates and tabs, power protection components, cabinets, and enclosures
- Oil and Gas: Connectors, fasteners, brackets, clips, tabs, valves, and metal parts in equipment for oil and gas drilling and exploration applications
- Medical: Parts for implantable pumps and valves, surgical instrumentation, or hardware and panels used in large equipment and furnishings
- Construction: Connectors and fasteners for trusses and framing, braces, brackets, cover plates, and enclosures used in systems throughout buildings
- Industrial Machinery: Components in engines and heavy equipment, tiny parts for electrical systems in machinery, and panels for equipment cabinets
Metal Stamping Services From Keats Manufacturing
Keats Manufacturing has been a leader in the precision metal stamping industry since 1958. We are ISO:9001, ISO:14001, and IATF:16949 certified, with three full-service facilities in North America.
Frequently Asked Questions
What industries benefit from metal stamping?
At Keats Manufacturing Co., we serve a diverse range of industries that benefit from our custom precision metal stamping services.
- Our high-volume solutions are ideal for the automotive and electronics sectors.
- With extensive capabilities, we maintain high precision tolerances of ±0.0002 in.
- Our ISO 9001 and IATF 16949 certifications ensure that all products meet stringent industry standards.
How does metal stamping work?
Metal stamping is a manufacturing process that transforms flat metal sheets into desired shapes using dies and presses.
- At Keats Manufacturing Co., we utilize one of North America's largest fleets of four-slide machines, including unique Wünsch multi-slide machines.
- Our in-house tool & die development ensures efficiency and precision, backed by a lifetime guarantee.
- This process allows for rapid production rates, making it suitable for high-volume applications.
What materials can be used in metal stamping?
Keats Manufacturing Co. works with a variety of materials for our metal stamping services, tailored to your project needs.
- Common materials include stainless steel, aluminum, brass, bronze, and copper, each selected for their specific attributes.
- Our extensive experience allows us to guide you in choosing the best materials for your project.
What are the advantages of precision metal stamping?
Precision metal stamping offers several advantages that Keats Manufacturing Co. leverages for our clients.
- High-volume production with consistent precision, achieving tolerances of ±0.0002 in.
- Cost-effective manufacturing, reducing waste and lead times through our advanced machinery.
- Our state-of-the-art facilities in IL, TX, and Mexico enable us to meet diverse project demands efficiently.
Can Keats Manufacturing Co. handle custom designs?
Yes, Keats Manufacturing Co. specializes in custom metal stamping solutions tailored to your specifications.
- Our in-house engineering team collaborates closely with clients to develop unique designs.
- With our advanced tool & die development capabilities, we ensure a seamless transition from concept to production.
- We guarantee precision and quality with our lifetime tool guarantee, giving you peace of mind.
How does Keats ensure quality in metal stamping?
Quality is a top priority at Keats Manufacturing Co., and we implement rigorous standards to ensure it.
- We are certified to ISO 9001, ISO 14001, and IATF 16949, ensuring adherence to international quality standards.
- Our extensive quality control process includes precision inspections and testing throughout production.
What is the lead time for metal stamping projects?
Lead times at Keats Manufacturing Co. vary based on project complexity and volume requirements.
- Our efficient in-house tool & die development enables quicker turnaround times for custom projects.
- Generally, we aim to deliver high-volume orders promptly without compromising quality, often within weeks.
- Contact us for a tailored quote based on your specific needs and timelines.
What sets Keats apart from other metal stamping companies?
Keats Manufacturing Co. stands out due to our extensive capabilities and commitment to quality.
- We own one of the largest fleets of four-slide machines in North America, allowing for versatile production options.
- Our in-house tool & die development, backed by a lifetime guarantee, ensures top-notch precision.
- With our strategic facilities in IL, TX, and Mexico, we deliver high-quality solutions to meet diverse industrial needs.
With expertise in four-slide, multi-slide, and progressive metal stamping, we can manufacture custom stampings to meet your application needs. Please contact us to speak with a member of our team, or request a quote today.